Production model
Hybrid by design: outsource fabrication, own the proof
Printed circuit boards are fabricated and populated through qualified surface-mount partners. Everything that decides whether a product actually works — programming, through-hole insertion, coating, enclosure assembly, testing and burn-in — happens on our line.
It is a deliberate boundary. Interoperability is proven at our bench rather than assumed from a supplier report, and changeover between SKUs costs labour hours instead of a stencil and feeder reset. The gate for bringing SMT in-house is sustained volume and demonstrated yield, not preference.
Start lean
No surface-mount line to staff, calibrate and maintain before the first order ships; capability is added when utilization justifies it.
Control where value lives
Every unit is flashed, tested and burnt in by us, with results logged against its serial.
Built to flex
Multi-SKU, low-to-mid volume production with fast changeover and duplicate test cells.
Workflow
Nine stations from incoming QC to dispatch
Each station has a written acceptance criterion and produces a record. A unit that cannot prove its last station cannot leave the building.
Incoming QC
PCBA and component inspection, AOI report review, solderability sampling and authenticity checks on long-lead parts.
Store & kitting
Moisture-sensitive-device controlled store, FIFO discipline on electrolytics, barcode kit issued per work order.
TH insert & wave solder
Transformers, terminals and chokes inserted and soldered, flux cleaned, joints inspected to workmanship standard.
Flash & configure
Firmware checksum verified, serial and short-address programming, identity label printed and bound to the unit.
Coat or pot
Conformal coating or potting for IP-rated variants with controlled cure, thickness and coverage verification.
Enclosure build
Case assembly, thermal pad placement, cable gland and strain relief fitting, torque-controlled fastening.
End-of-line test
100% test: hi-pot, power accuracy, protocol communication, dimming curve and colour performance on every unit.
Burn-in & final QC
Six to eight hours at 60 °C, full re-test after soak, cosmetic and label audit, then packing.
Dispatch & trace
Carton serials written to MES, warranty register opened, dispatch against project schedule or stock policy.
Quality system
Five stages of proof
Sampling where risk is statistical; 100% where a single escape becomes a project-level liability.
Incoming QC — sampled
AOI reports, component authenticity, solderability sampling on every incoming lot.
In-process — every board
Flash checksum, joint inspection, coating cure verification.
End-of-line — 100%
Safety, power accuracy, protocol communication, dimming and colour.
Burn-in — 100%
6–8 hours at 60 °C followed by a complete re-test.
Reliability audit — sampled
Surge, 85/85 humidity and thermal imaging on production parts.
95%
First-pass yield by month 3
98%
First-pass yield by month 6
<500
DPPM field-failure target at 12 months
5yr
Warranty register per project batch
Traceability is the defence
Serial number, device address and firmware checksum are logged to MES for every unit, linked to component lots and test results. When a five-year fixture warranty claim arrives, the exact build that produced that unit can be reconstructed — and the population at risk can be bounded.
- IPC-A-610 workmanship standard as the acceptance reference
- ESD-safe EPA flooring, controlled humidity, MSD dry cabinets
- Annual calibration programme for all measurement instruments
- Dual test and wave-solder cells for redundancy at peak output
Plant infrastructure
Sized for 1,000 to 3,000 units a day
10,000–15,000 ft²
Assembly, test, stores and dispatch in a single supervised flow with clear personnel and material routes.
150–250 kVA
Dedicated power with metering per line, UPS for test and programming stations, surge protection at entry.
60 °C burn-in room
500 to 1,000 positions with programmable soak profiles and per-position electrical monitoring.
Calibrated test lab
Safety analysers, programmable sources, power meters and protocol rigs maintained on a scheduled calibration cycle.
Equipment
What the line is built from
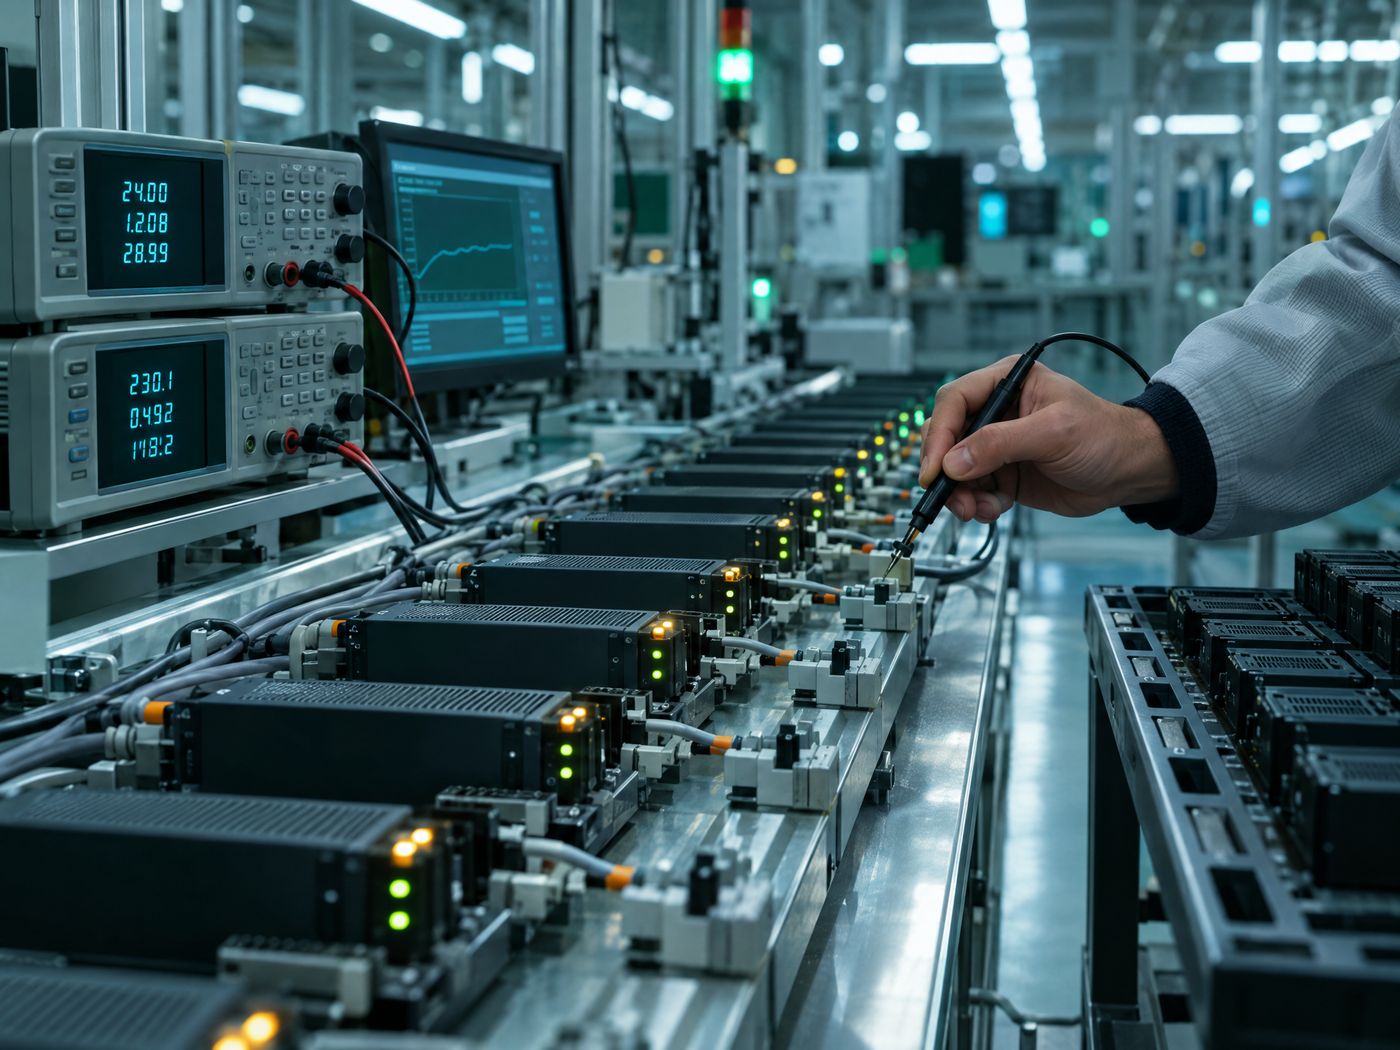
Test and burn-in account for roughly 35–40% of the equipment on the floor. That proportion is deliberate: assembly capacity is easy to add, proven quality is not.
- Wave soldering line with fluxer and joint inspection stations
- Through-hole insertion and component forming stations
- Firmware flashing and protocol configuration stations
- Conformal coating and potting line with controlled cure oven
- Enclosure assembly jigs, presses and torque-controlled drivers
- Label printing and thermal inkjet coding with serial binding
- End-of-line test benches with product-specific fixtures
- Hi-pot, ground-bond and leakage safety testers
- Power analysers and programmable AC sources
- Protocol test rigs and sequencer PCs running automated scripts
- Burn-in racks and 60 °C soak room, 500–1,000 positions
- MES and ERP integration for serial-level traceability
Certification
Certified as a product, verified independently
Protocol certification derives from published device test specifications, not from a factory inspection. Test sequences run on approved equipment, results are submitted per model and are independently verified before a listing is issued.
- 1
Test specifications obtained
Sequences derive from published parts of the device standard, not from a plant audit.
- 2
Each model tested in-house first
Approved-class rigs run the full sequence on our bench before any submission.
- 3
Accredited test house run
Booked before the pilot build so re-test loops do not consume a quarter.
- 4
Results submitted per product
One submission per model with the required membership in good standing.
- 5
Independent verification
The certifying body checks the submission itself — the difference from self-declared claims.
- 6
Public listing and logo rights
The model appears in the public product database while membership remains active.
Ramp-up
180 days from lease signature to certified dispatch
Phase 1 · Days 0–30
Mobilise
- Facility lease, layout, power and ESD fit-out
- Certification body membership application filed
- Two SMT partners qualified and audited
- BOM and approved vendor list locked
Phase 2 · Days 30–90
Install & pilot
- Equipment installation and calibration
- SOPs, jigs and work instructions released
- Pilot lot of 200 units built
- Internal pre-compliance run
Phase 3 · Days 90–150
Certify
- Safety registration filings
- Independent protocol certification run
- Customer PPAP samples submitted
- Burn-in policy live and enforced
Phase 4 · Days 150–180
Scale
- Start of production
- First certified SKUs ship
- Yield driven to 95%
- In-house SMT investment review
Timeline assumes design freeze is already achieved and a single greenfield site in an industrial estate.
Risk control
Six production risks, six standing mitigations
Risk 01
Component dependency
Electrolytics, magnetics and transceivers are largely imported; one single-source part can stop a line.
→ Dual-source from qualification; 8–12 weeks cover on long-lead lines.
Risk 02
Certification timing
Test-house queues and re-test loops can consume a quarter before the first certified SKU ships.
→ Join early, pre-test internally, book the slot before the pilot build.
Risk 03
Scarce protocol talent
Few engineers have commissioned real addressable lighting networks; the training burden sits with us.
→ Hire test engineers first; automate sequences so operators can run them.
Risk 04
Warranty exposure
Drivers fail first inside a five-year fixture warranty; a bad batch becomes a project liability.
→ 100% burn-in, 85/85 sampling and a standing warranty reserve.
Risk 05
Uncertified competition
Cheap "compatible" imports undercut on price and blur the category for specifiers.
→ Sell certification: quote the public product-database listing in every tender.
Risk 06
Revision drift
Firmware and component changes drift silently; a fielded batch must stay traceable to its build.
→ Checksum gate at flashing, serial-level MES, engineering-change lock.
Audience: OEMs, EPC contractors and smart-city tenders
Bring a bill of materials, a target volume and a warranty term. We will tell you which stations your product needs and what the line must prove before it ships.